Contact us

2026 Best Peripheral Drive Thickeners for Global Buyers?

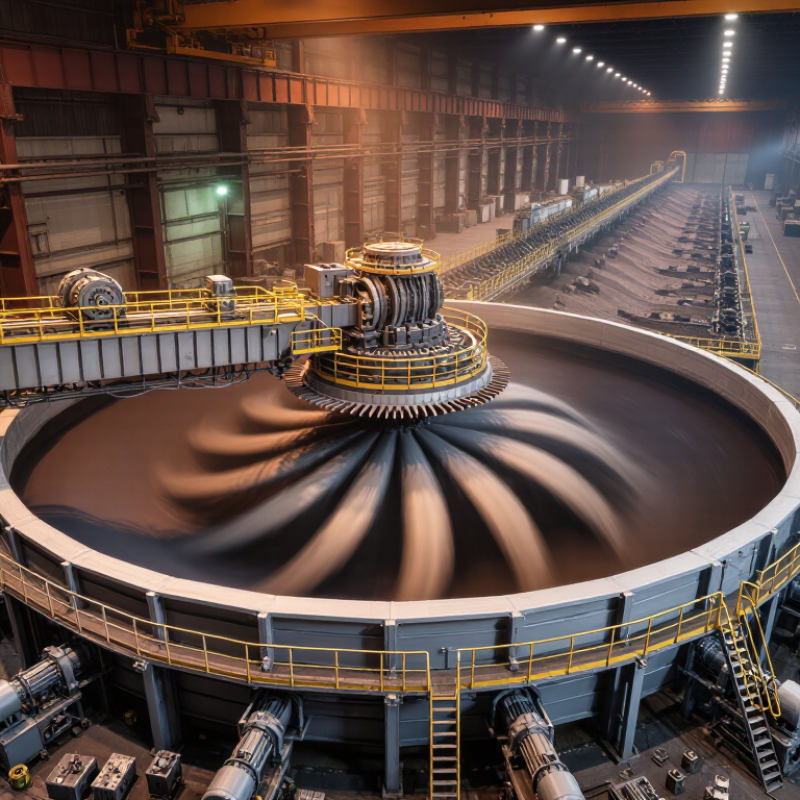
Global buyers are reassessing water recovery, underflow density, and maintenance risk in mineral processing plants. The Peripheral Driving Thickener has become an important option for large-volume clarification and tailings applications. Its rotating rake mechanism moves settled solids toward the discharge cone, while the peripheral drive supports controlled torque transmission around the tank edge.

Market reports show why this equipment deserves closer evaluation. Grand View Research estimates that the global mining equipment market reached approximately USD 135.9 billion in 2023. Its forecast also indicates continued growth through 2030. However, most market studies do not separately measure peripheral-drive thickeners. That gap matters. Buyers should avoid treating broad equipment statistics as direct proof of demand.

Professor Fernando Concha, a recognized authority on sedimentation and thickening, offers a practical reminder: “Thickening is a process decision before it is an equipment decision.” The quotation captures a common purchasing mistake. Tank diameter alone cannot predict performance. Ore type, flocculant response, feed solids, settling velocity, and underflow targets require testing.

A 30-meter tank may look impressive. It may still underperform with unstable feed chemistry. Buyers should compare torque capacity, rake-lift protection, drive redundancy, bridge design, instrumentation, and local service support. Metso, FLSmidth, and other established suppliers publish technical guidance, but supplier data still requires independent review.

There is no universal best model. Not yet.

The strongest 2026 shortlist will combine pilot results, lifecycle cost analysis, documented references, and realistic site conditions. That approach is slower, but usually more reliable.
2026 Best Peripheral Drive Thickeners for Global Buyers?

What Are Peripheral Drive Thickeners and How Do They Work?

2026 Best Peripheral Drive Thickeners for Global Buyers?

Peripheral drive thickeners use gravity to separate water from sludge. A circular tank holds the feed, while a rotating bridge moves rake arms across the floor. These rakes guide settled solids toward the central hopper. Clarified liquid rises and exits through an overflow weir. The drive unit sits near the tank perimeter, reducing shaft stress and leaving the center open for feeding. Simple, but not effortless.

Operators should watch solids capture, overflow rate, torque, and underflow concentration. A well-designed feedwell slows incoming sludge and limits turbulence. Rake teeth then create channels for trapped water to escape. Typical sludge may leave at roughly 2% to 6% total solids, depending on feed type and polymer control. The U.S. EPA’s 2022 Clean Watersheds Needs Survey estimated $630.1 billion in wastewater infrastructure needs. That figure shows why energy-efficient, maintainable thickening equipment matters to global buyers.

The Water Environment Federation’s Manual of Practice No. 8 emphasizes process testing before equipment selection. Tank diameter alone does not prove performance. Climate, sludge age, temperature, and operator skill can change results. The word “best” is uncomfortable here. A peripheral drive thickener may perform poorly when torque protection is weak or rake clearance is ignored. Buyers should request pilot data, corrosion specifications, emergency-stop details, and measured underflow results. Do not trust a perfect brochure. Field conditions are rarely perfect.
2026 Best Peripheral Drive Thickeners for Global Buyers

Peripheral drive thickeners use a drive mechanism mounted at the tank rim to rotate the bridge and rake arms. As suspended solids settle, the rake system guides thickened sludge toward the central underflow outlet while clarified liquid flows over the peripheral weir.

Indicative industry ranges shown as mass percentage of slurry. Actual feed and underflow concentrations depend on material properties, flocculant selection, tank geometry, rake design, and operating conditions.

Key Design Features and Performance Factors to Compare

2026 Best Peripheral Drive Thickeners for Global Buyers?

A peripheral drive thickener should be judged by more than tank diameter. The drive unit must deliver steady torque under uneven sludge loading. A wide-diameter basin can hide weak rake-arm design. Ask for torque calculations, overload protection, and corrosion-resistant materials. The feedwell should distribute sludge gently, without short-circuiting flow. Scraper blades must move settled solids toward the withdrawal hopper. Small design details matter.

The U.S. EPA’s Wastewater Technology Fact Sheet on Gravity Thickening reports that gravity thickening can raise sludge concentration to roughly 2–5% solids. It also identifies potential volume reductions of about 50–80%. These figures depend heavily on sludge type, temperature, and operator control. They are not guaranteed results. The Water Environment Federation’s Manual of Practice No. 8 emphasizes solids loading, hydraulic loading, detention time, and overflow performance during design review. Buyers should request test data using representative sludge, not clean water.

Performance monitoring should include underflow solids, overflow suspended solids, rake torque, and polymer demand where applicable. Variable-speed drives can help manage changing feed conditions. Remote alarms are useful, but sensors still need cleaning and calibration. Check seals, gearbox access, walkway safety, and spare-part availability in the destination country. For coastal or tropical sites, coating systems and stainless components deserve closer review. I would also compare energy data at partial load. Full-load figures can look impressive, yet daily operation is rarely so neat.

2026 Best Peripheral Drive Thickeners for Global Buyers? - Key Design Features and Performance Factors to Compare
Thickener Configuration Typical Basin Diameter Typical Side Water Depth Typical Rake Speed Indicative Solids Loading Range Indicative Underflow Solids Drive and Torque Features Preferred Application Key Selection Considerations
Conventional peripheral-drive thickener 15–60 m 2.5–4.5 m 0.03–0.10 rpm Approximately 50–150 kg/m²·d, depending on feed characteristics Approximately 2–8% dry solids for many mineral and industrial slurries Rim-mounted drive with slow-speed gear reduction; overload protection and torque monitoring are essential Large municipal, mineral-processing, and industrial wastewater duties Verify feed flocculation, settling tests, torque margin, bridge stiffness, and local wind loads
High-rate peripheral-drive thickener 10–45 m 3.0–6.0 m 0.02–0.08 rpm Approximately 100–300 kg/m²·d with suitable feed conditioning Approximately 3–12% dry solids, subject to slurry rheology Higher torque capacity, variable-frequency control, robust rake-lift arrangement, and automatic overload shutdown Applications requiring a smaller footprint and higher throughput per unit area Compare flocculant demand, bed compression behavior, feedwell design, and peak torque under upset conditions
Deep-bed peripheral-drive thickener 12–40 m 5.0–10.0 m 0.01–0.06 rpm Approximately 150–400 kg/m²·d for suitable mineral or industrial slurries Approximately 8–25% dry solids, depending on compression and material properties High-torque peripheral drive, heavy-duty rake arms, rake-lift protection, and continuous torque measurement Mineral concentrates, tailings, backfill feed, and high-solids industrial slurries Confirm compression testing, yield stress, rake clearance, emergency lifting capacity, and underflow pumping requirements
High-compression peripheral-drive thickener 8–30 m 6.0–12.0 m 0.005–0.04 rpm Approximately 200–600 kg/m²·d in selected mineral applications Approximately 15–35% dry solids, highly dependent on solids mineralogy Very high starting and running torque; requires reinforced rake structure, torque-limiting devices, and reliable rake-lift control High-density underflow duties where water recovery and compact plant layout are priorities Use pilot testing to establish compression rate, bed height, residence time, and achievable underflow density
Stainless-steel or corrosion-resistant peripheral-drive thickener 8–35 m 2.5–6.0 m 0.02–0.10 rpm Approximately 50–250 kg/m²·d, based on the process slurry Approximately 2–15% dry solids Drive arrangement is similar to standard units; wetted components may use stainless steel, coated carbon steel, or corrosion-resistant alloys Food, chemical, mining, and wastewater streams with corrosive or hygienically sensitive liquids Compare chloride resistance, coating system, galvanic compatibility, inspection access, and lifecycle maintenance cost
Clarifier-thickener combination with peripheral drive 15–70 m 2.5–5.0 m 0.03–0.10 rpm Approximately 30–150 kg/m²·d Approximately 1–8% dry solids Moderate-speed rim drive with scraper or rake assembly; requires stable rotation and dependable scum or floating-solids handling where applicable Municipal and industrial wastewater treatment with simultaneous clarification and sludge thickening Compare hydraulic surface loading, solids retention time, overflow quality, sludge blanket control, and scum removal provisions
Covered peripheral-drive thickener 10–45 m 2.5–8.0 m 0.01–0.08 rpm Approximately 50–300 kg/m²·d Approximately 3–20% dry solids Drive must accommodate roof loads, restricted access, ventilation requirements, and safe maintenance procedures Odor-controlled wastewater plants and processes requiring protection from rain, snow, or freezing Assess roof structure, ventilation, hazardous-area classification, access platforms, and climate-specific corrosion protection
Note: The figures are typical preliminary-design ranges rather than guaranteed performance values. Final sizing and drive selection should be based on slurry characterization, laboratory or pilot settling tests, rheology, solids loading, climate, structural design, and applicable local standards.

How to Select the Right Model for Different Industries

2026 Best Peripheral Drive Thickeners for Global Buyers?

Selecting a peripheral drive thickener starts with sludge behavior, not catalogue capacity. Municipal sludge often needs steady hydraulic flow and moderate rake torque. Food-processing sludge may contain grease, fibers, and rapidly changing solids. Mining applications can demand higher torque, abrasion resistance, and reinforced rake arms. Pulp and paper sludge behaves differently again.

Use measured data from representative samples. Key inputs include feed solids, settling velocity, peak flow, underflow concentration, and polymer demand. WEF Manual of Practice No. 8 recommends evaluating solids flux and hydraulic loading together. A thickener sized only by daily flow can fail during storm inflow. It happens. Check torque margins, rake-lift protection, corrosion resistance, and access for cleaning.

Budget planning also matters. The U.S. EPA’s 2023 Clean Watersheds Needs Survey estimates $630.1 billion in national wastewater infrastructure needs over 20 years. Energy and maintenance choices therefore deserve early attention. UN-Water’s 2024 World Water Development Report notes that agriculture uses about 70% of global freshwater withdrawals. Food and agricultural plants may value water recovery and stable underflow more than maximum throughput. Coastal sites need stronger material protection, while cold regions need freeze-resistant instrumentation. Pilot testing remains the safer decision. Laboratory results can mislead when sludge ages, temperature, or polymer quality changes. The uncomfortable question is simple: does the selected model match tomorrow’s feed, not only today’s sample?

Global Buyer Guide to Materials, Standards, and Suppliers

2026 Best Peripheral Drive Thickeners for Global Buyers?

For global buyers, material selection should match slurry chemistry, climate, and maintenance access. Carbon steel with protective coating suits many municipal applications. Stainless steel 304 or 316 is safer for corrosive process water. FRP components can reduce corrosion, but they need careful structural review. I have seen failures caused by choosing materials from water samples alone.

Drive sizing deserves equal attention. Ask for torque calculations, rake-load data, overflow rates, and emergency stopping performance. A thickener operating at high altitude may need different motor and cooling provisions. Seals, bearings, scraper arms, and bridge structures should be inspected through a clear maintenance plan. Small details matter.

Standards improve supplier comparison. Request material certificates, weld inspection records, coating specifications, and documented factory testing. ISO 9001-based quality systems can support traceability, but certification alone proves little. Confirm applicable EN, ASTM, or ISO requirements with the project engineer. Electrical protection must also match local regulations and site conditions. Suppliers should provide drawings, manuals, spare-parts lists, and remote commissioning support. Ask about lead times honestly. Delays happen. A complete technical offer is more valuable than a low initial price. My own preference is a supplier that admits design limits and records every change before production.

Installation, Maintenance, and Total Ownership Considerations

2026 Best Peripheral Drive Thickeners for Global Buyers?

Installation & Testing

Installation determines whether a peripheral drive thickener performs reliably. Check the tank rim level before placing the bridge and drive assembly. Even a small elevation error can increase scraper load. Measure twice. Anchor bolts need controlled tightening, not excessive force. After alignment, rotate the mechanism without load and listen for rubbing, vibration, or uneven resistance. Record motor current during this test. These readings create a useful baseline for future inspections.

Maintenance & Reliability

Maintenance should match the site’s sludge quality and climate. Inspect wheels, tracks, seals, scraper arms, and torque protection each week during early operation. Remove grit and hardened sludge before it reaches moving components. Keep it clean. Lubricate bearings according to the equipment manual, while avoiding over-greasing near seals. In humid or coastal areas, inspect exposed steel for coating damage. A neglected wheel can damage the track quickly. In practice, maintenance teams sometimes trust visual checks too much; vibration trends often reveal trouble earlier.

Total Ownership Cost

Total ownership cost includes more than purchase price. Compare energy use, replacement wheels, scraper wear parts, lubricants, labor, transport, and planned downtime. Ask whether common components are available near the installation site. Local technical training may reduce long service delays. Keep spare seals and critical fasteners on site. A cheaper thickener can become expensive after one unplanned shutdown. However, energy estimates may change with sludge concentration, temperature, and daily flow, so buyers should verify assumptions using operating data rather than relying only on supplier calculations.